
3D printing problems is a decision that sits at the intersection of design, material, process capability and commercial terms. Buyers asking about printing process failure modes usually want a part that fits, looks right, arrives on time and can be reordered without drama. Getting there depends on how clearly the requirement is written before any metal is cut.
This guide sets out what a complete 3D printing problems specification contains, how suppliers actually price it, and which drawing notes prevent the disputes that cost the most. It is written for purchasing teams and design engineers working on custom additive parts in thermoplastic and resin, rather than for machine operators.

What 3D printing problems Really Means for a Buyer
3D printing problems is a phrase that appears in enquiries long before anyone agrees what work it covers. For a purchasing team it describes a set of decisions about printing process failure modes, not a single operation. Getting those decisions written down early is what separates a clean first article from a dispute about scope three weeks later.
In practice the term spans design intent, material condition, process capability, inspection method and commercial terms. A supplier reading the same words may assume a different route, a different tolerance band or a different level of documentation. The 3D printing problems conversation should therefore start with a written definition of the deliverable rather than a price request.
This guide is written for buyers and design engineers who specify printing process failure modes on custom additive parts made from thermoplastic and resin. It sets out the questions that change cost, the drawing notes that prevent ambiguity, and the checks that make a 3D printing problems quotation comparable between suppliers.
The 3D printing problems Process Step by Step
A typical route begins with a drawing review, then material preparation, the primary forming or cutting operation, secondary operations, finishing, cleaning and finally inspection. Each handover is a place where a requirement can be lost, which is why a route card is more useful than a verbal description when discussing 3D printing problems.
The primary operation establishes the geometry, but the secondary steps usually determine whether the part is usable. Deburring, heat treatment, surface finishing and masking all add time and can change a dimension. Ask the supplier to list every step in the 3D printing problems route, including the ones they consider routine.
Holding points matter as much as the steps themselves. A first-article check after the primary operation catches a tooling problem before finishing hides it, and a final check against the approved sample closes the loop. For 3D printing problems projects, agree these points before the order is released.
Materials and How They Behave
Material choice drives almost every downstream decision in 3D printing problems. thermoplastic and resin behaves differently under cutting heat, forming pressure and finishing media, and those differences show up as tool wear, distortion, surface texture and achievable tolerance. A grade that is easy to machine may be poor for the service environment.
Ask for the exact grade, condition and, where relevant, the mill certificate. Equivalent grades from different regions are not always interchangeable, and a substitution made after quotation breaks traceability. In a 3D printing problems enquiry, the material line on the drawing should be specific enough to order from without a phone call.
Stock form matters too. Bar, plate, casting, sheet and powder each carry their own residual stress and surface condition. A part machined from stressed plate can move after material is removed, so a stress relief or roughing step may be needed. That is a 3D printing problems cost driver, not a detail to discover at inspection.
Design Rules That Affect 3D printing problems
Geometry decides how many setups, tools and fixtures a part needs. Deep pockets, thin walls, undercuts, sharp internal corners and features on several faces all add operations. Simplifying those features while keeping function intact is the cheapest way to reduce 3D printing problems cost, and it rarely requires a performance compromise.
Tolerances should be assigned where they matter, not applied uniformly. A blanket general tolerance forces the supplier to treat every dimension as critical, which changes the process plan and the inspection time. Mark the functional datums and bounding features explicitly, then let the rest of the 3D printing problems drawing carry a sensible default.
Consider access. A cutter, a probe, a blasting nozzle or a coating spray must physically reach the surface it is meant to treat. Features hidden behind a boss or inside a blind cavity often need a special tool or a secondary setup. Reviewing access early is a standard part of a 3D printing problems design review.
| Decision | What to specify | Why it matters |
|---|---|---|
| Material | Exact grade, condition, certificate | Controls behaviour and traceability |
| Tolerance | Datums, characteristic, method | Makes the requirement measurable |
| Finish | Process, direction, reference sample | Prevents cosmetic disputes |
| Inspection | FAI, in-process, final plan | Sets cost and holding points |
| Scope | Tooling, finishing, packaging | Keeps quotations comparable |
Tolerances, Measurement and Inspection
A tolerance without a measurement method is an opinion. State the datum scheme, the characteristic being controlled, the instrument and the number of reading points. For 3D printing problems, also define whether dimensions apply before or after finishing, because a coating or a polishing pass can move a size by several micrometres.
Geometric tolerances deserve the same attention as size. Flatness, perpendicularity, position and runout are frequently the real functional requirements, yet they are omitted from a drawing that only lists plus and minus values. A clear 3D printing problems inspection plan names each geometric callout and how it will be verified.
Agree the sampling plan before production. First-article inspection, in-process checks and final lot acceptance are different activities with different costs. Recording the approved settings makes a 3D printing problems order reproducible months later when the part is reordered or the tool is refurbished.
Supplier capacity is a quiet schedule risk. A shop can quote accurately and still be unable to hold the date if a larger customer takes the machine time. Asking about realistic capacity for the expected volume of additive parts is more useful than accepting an optimistic promise.
Tool wear is a gradual drift rather than a sudden failure. Cutting edges, dies, belts and media all degrade, and the part slowly moves toward a tolerance limit. Define a tool change interval or a control chart trigger so the drift is caught while parts are still inside the band.
Drawing revision control sounds administrative until two versions reach the shop. Mark the revision clearly, require acknowledgement of the latest issue, and ask the supplier to confirm which revision their quotation and tooling were built against. This is especially important after a design freeze.
Failure analysis is most useful when it is structured. Rather than assigning blame, record the symptom, the process step, the measurement, the likely cause and the corrective action. A short report of this kind turns a single rejected batch of additive parts into a permanent process improvement.
Storage conditions between operations are frequently overlooked. thermoplastic and resin can pick up moisture, oxide or contamination while a batch waits for its next step, and that changes how the following operation behaves. A covered, segregated holding area with a time limit is a cheap control.
Environmental conditions in the workshop affect results more than most drawings acknowledge. Temperature changes a measured length, humidity changes a coating cure, and airborne dust changes a cosmetic finish. State the conditions under which the acceptance measurement is taken.
Cleanliness requirements vary enormously by industry. Medical, optical, food and semiconductor parts may need particulate limits, certified cleaning and clean packaging, while general industrial parts do not. State the requirement explicitly; assuming a standard shop clean is a common source of rejection.
Surface Finish and Appearance
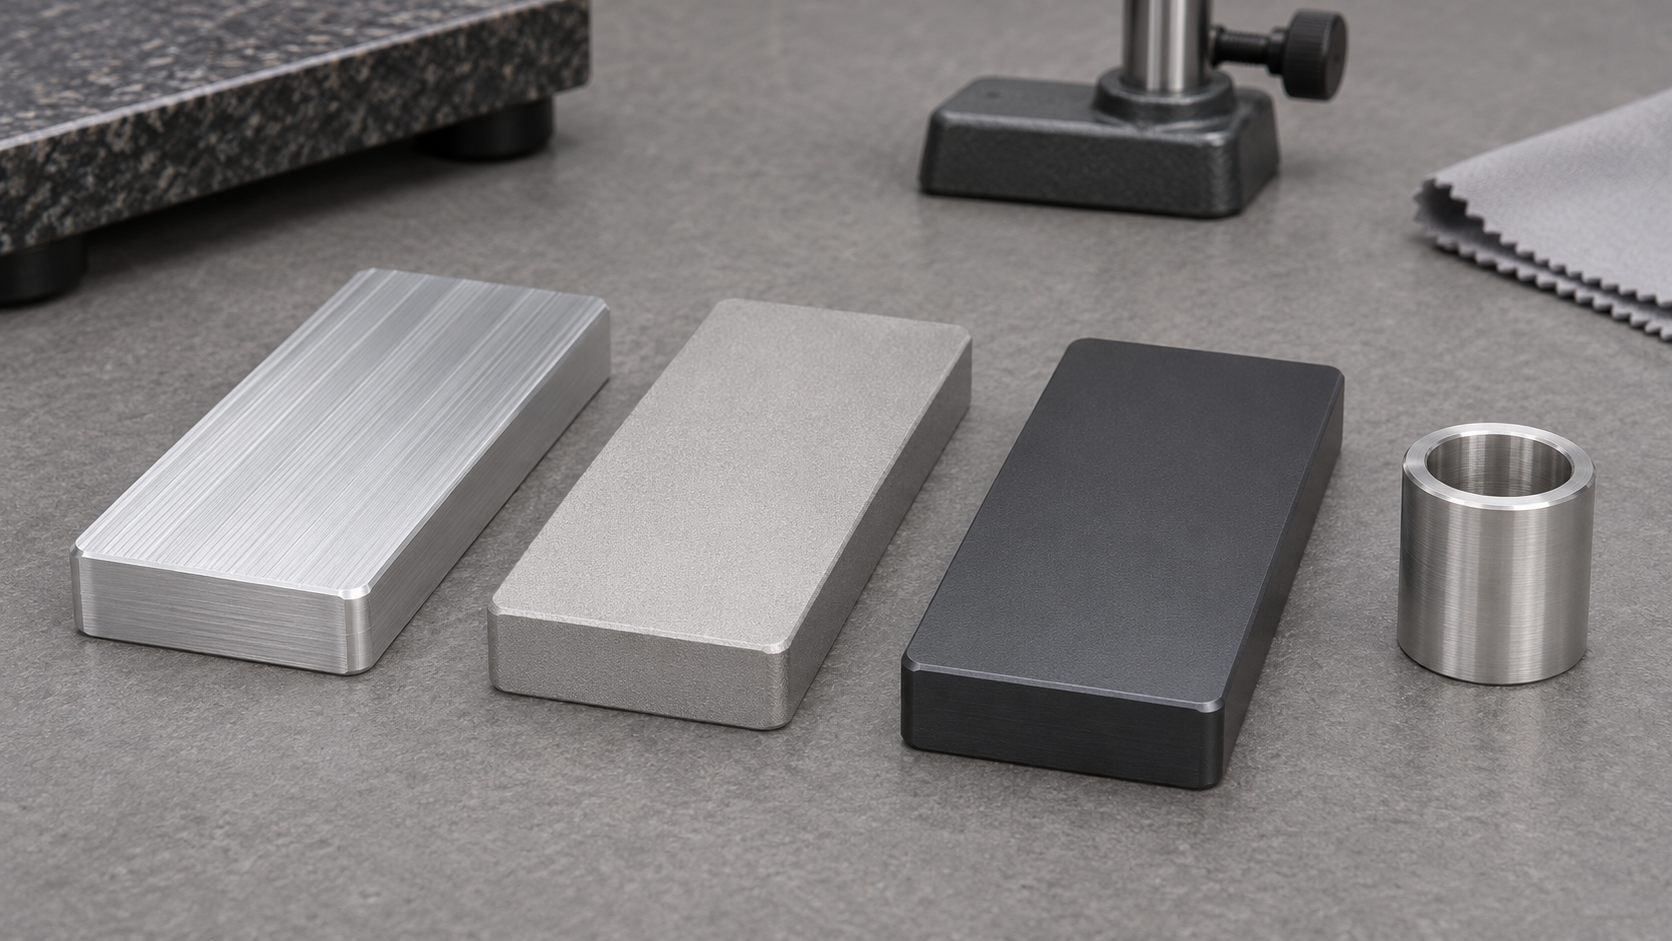
Surface requirements cover roughness, lay, visual class and coating condition. A single Ra number rarely captures what a buyer actually wants, because two surfaces with the same Ra can look completely different. Specify the process, the direction of any grain and a physical reference sample for 3D printing problems.
Finishing is the last operation but not the last variable. Handling, packaging and assembly can mark a cosmetic face far more easily than a functional one. Include protection in the 3D printing problems specification and in the quotation rather than relying on a verbal instruction at dispatch.
If a coating follows, the substrate preparation decides adhesion. Cleaning, degreasing, conversion layers and the interval between preparation and coating all need limits. A complete 3D printing problems chain treats the finish as a system, not as a decorative afterthought.
Finally, keep a short lessons-learned note after the first production batch. Record what was quoted, what actually drove cost, which drawing note prevented a problem, and what would change next time. That note makes the second order of additive parts faster and cheaper for everyone involved.
First-article approval is a decision point, not a formality. The sample should be made with the intended production material, tooling and finishing route, then measured against every drawing callout. Keeping that sample as a physical reference removes ambiguity from later discussions about additive parts.
Quantity breaks are a commercial detail with an engineering cause. Setup, programming, tooling and first-article inspection are fixed costs spread over the batch, while material and cycle time scale with each piece. Understanding that split makes a price curve readable rather than mysterious.
Design for assembly is easy to forget when reviewing a single component. A part that is correct in isolation can be difficult to fit, align or fasten once it reaches the assembly line. Checking the mating part drawing and the assembly sequence early avoids a late engineering change.
Fixture design is an engineering deliverable in its own right. A well designed fixture locates on the same datums used for inspection, avoids clamping on a functional face, and allows the operator to load a part the same way every cycle. Ask to see the concept before tooling is cut.
Subcontracted steps need the same control as in-house ones. Heat treatment, plating, anodising and specialist inspection are often outsourced, and each handover adds transport time and a documentation gap. Name the approved subcontractor and require its certificate with the shipment.
Tooling, Setup and Lead Time
Some routes need dedicated tooling, others only standard fixtures and a program. Tooling cost, tool life and who owns the tool are commercial questions that belong in the 3D printing problems quotation, not in an appendix discovered after approval. Ask for the amortisation method explicitly.
Setup time dominates small batches while cycle time dominates large ones. That is why a unit price falls with quantity but the first article still carries a fixed cost. Understanding this split helps a buyer compare 3D printing problems quotes across different order quantities without being misled by a headline number.
Lead time should be broken into material procurement, programming or tool making, first article, production and finishing. A single promise of four weeks hides where the risk sits. For 3D printing problems planning, request the milestones and the conditions that would move them.
Packaging and handling deserve the same attention as the operation itself. A batch of additive parts that passes inspection can still arrive marked if it is stacked unprotected, so specify separators, caps or individual wrapping where the surface matters. This is a small cost that prevents a disproportionate number of rejections at goods inward.
Rework rules are worth agreeing before they are needed. Some nonconformances can be corrected by a second pass, while others change a dimension or a surface irreversibly. A written rule that names who authorises rework and how it is recorded avoids an informal decision under schedule pressure.
Freight and incoterms belong in the comparison. A lower unit price can be erased by packaging, export documentation, insurance or an unfavourable delivery term. Ask every supplier to quote to the same delivery point so the numbers describe the same obligation.
Prototype intent and production intent are different documents. A prototype drawing may allow manual finishing and broad tolerances, while a production drawing needs defined processes and inspection. Mark which stage the current revision applies to so the shop does not guess.
Operator instructions should be written, not inherited. A route card that names the tool, the speeds, the coolant, the inspection point and the acceptance criterion is what makes a repeat order reproducible. Photographs of a correct setup are a useful supplement for additive parts.
Change control protects long-running parts. A new material lot, a replaced tool, a reassigned machine or a revised program can all shift the output. A simple clause requiring written notification before any such change prevents a silent variation from appearing months later on additive parts.
Cost Structure in 3D printing problems Quotations
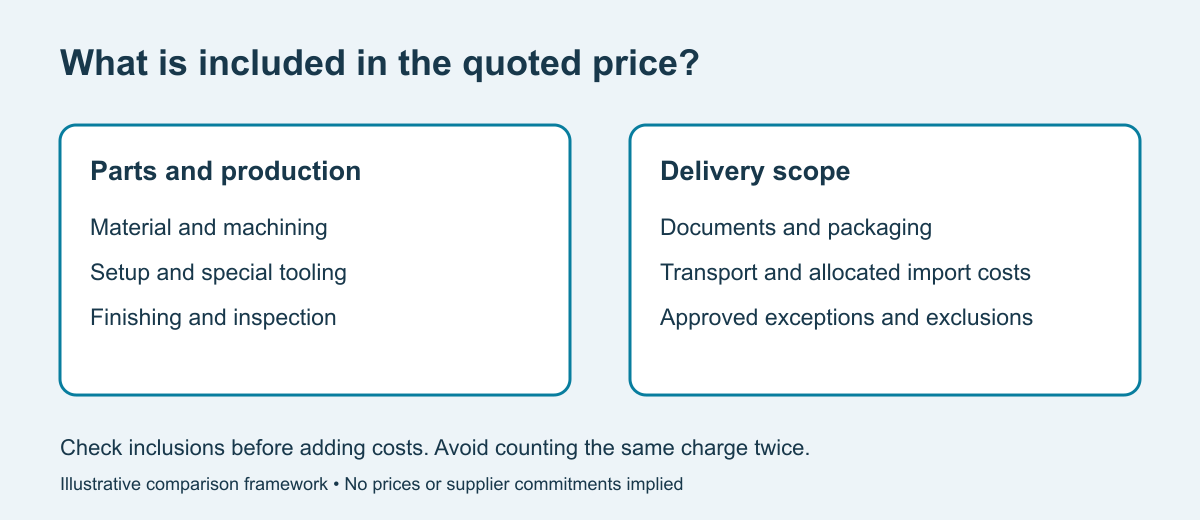
A useful quotation separates material, machine time, tooling, finishing, inspection, packaging and freight. When those are bundled into one figure, a lower price may simply be a narrower scope. Insist on a line-item breakdown before comparing 3D printing problems offers from different shops.
Hidden costs usually live in masking, cleaning, rework and documentation. A part with one cosmetic face and several critical bores needs plugs, tape and careful handling that a simple prismatic block does not. These are legitimate 3D printing problems costs, and hiding them only moves the disagreement to the invoice.
Volume changes the answer. A prototype may be cheaper by one route and a production lot by another, because setup and tooling amortise differently. Ask for price breaks at two or three quantities so the 3D printing problems decision can be made against the real demand pattern.
Communication during production is worth defining too. Agree who reports progress, at what milestones, and how a deviation is raised. A short written status note on additive parts is usually enough, and it prevents a schedule slip from becoming a surprise on the promised delivery date.
Measurement uncertainty matters when a tolerance is tight. An instrument with poor resolution, a worn stylus or an uncontrolled temperature can shift a reading enough to turn an acceptable part into a reject. Calibration records and a defined measurement environment are part of a credible inspection plan for thermoplastic and resin.
Payment terms and tooling ownership are often left out of technical discussions but decide real cost. Clarify whether tooling is amortised into the piece price, invoiced separately, or owned outright, and record who may use it for other customers. Ambiguity here creates problems on reorders of additive parts.
Supplier capacity is a quiet schedule risk. A shop can quote accurately and still be unable to hold the date if a larger customer takes the machine time. Asking about realistic capacity for the expected volume of additive parts is more useful than accepting an optimistic promise.
Tool wear is a gradual drift rather than a sudden failure. Cutting edges, dies, belts and media all degrade, and the part slowly moves toward a tolerance limit. Define a tool change interval or a control chart trigger so the drift is caught while parts are still inside the band.
Drawing revision control sounds administrative until two versions reach the shop. Mark the revision clearly, require acknowledgement of the latest issue, and ask the supplier to confirm which revision their quotation and tooling were built against. This is especially important after a design freeze.
Quality Systems and Documentation
Certificates, material traceability, inspection reports and process records cost money to produce but are essential in regulated or safety-critical supply chains. State which documents are required with each shipment. A 3D printing problems request that omits this often receives a price that excludes it by default.
Ask how nonconforming parts are handled: who decides rework, who carries the cost, and how a correction is documented. A documented corrective action is more valuable than an informal promise to be careful next time, particularly on repeat 3D printing problems orders.
For long-running parts, change control matters. A new material lot, a replaced tool, a moved operation or a subcontracted finishing step can all alter the result. A simple notification clause in the 3D printing problems agreement prevents silent changes that only appear as a field failure.
Storage conditions between operations are frequently overlooked. thermoplastic and resin can pick up moisture, oxide or contamination while a batch waits for its next step, and that changes how the following operation behaves. A covered, segregated holding area with a time limit is a cheap control.
Environmental conditions in the workshop affect results more than most drawings acknowledge. Temperature changes a measured length, humidity changes a coating cure, and airborne dust changes a cosmetic finish. State the conditions under which the acceptance measurement is taken.
Cleanliness requirements vary enormously by industry. Medical, optical, food and semiconductor parts may need particulate limits, certified cleaning and clean packaging, while general industrial parts do not. State the requirement explicitly; assuming a standard shop clean is a common source of rejection.
Finally, keep a short lessons-learned note after the first production batch. Record what was quoted, what actually drove cost, which drawing note prevented a problem, and what would change next time. That note makes the second order of additive parts faster and cheaper for everyone involved.
First-article approval is a decision point, not a formality. The sample should be made with the intended production material, tooling and finishing route, then measured against every drawing callout. Keeping that sample as a physical reference removes ambiguity from later discussions about additive parts.
Quantity breaks are a commercial detail with an engineering cause. Setup, programming, tooling and first-article inspection are fixed costs spread over the batch, while material and cycle time scale with each piece. Understanding that split makes a price curve readable rather than mysterious.
Common Defects and How to Prevent Them
Most recurring defects trace back to an undefined requirement rather than poor workmanship. Burrs, chatter, distortion, porosity, colour variation and coating adhesion failures all have clear process causes. Naming the acceptance criterion up front is the cheapest 3D printing problems prevention measure available.
Ask for the supplier’s own defect list for this part family. A shop that has made similar additive parts knows exactly where its process is sensitive, and will usually propose a fixture or a sequence change that removes the risk. That conversation is worth more than a generic quality promise.
Keep a retained sample of both an acceptable part and a rejected one. Photographs are unreliable because lighting and viewing angle change the reading, while physical limit samples give an inspector an unambiguous reference during 3D printing problems production.
Fixture design is an engineering deliverable in its own right. A well designed fixture locates on the same datums used for inspection, avoids clamping on a functional face, and allows the operator to load a part the same way every cycle. Ask to see the concept before tooling is cut.
Subcontracted steps need the same control as in-house ones. Heat treatment, plating, anodising and specialist inspection are often outsourced, and each handover adds transport time and a documentation gap. Name the approved subcontractor and require its certificate with the shipment.
Traceability is cheap to specify and expensive to retrofit. If a certificate, a lot number or a serial mark is needed, it must be captured at the time of manufacture rather than reconstructed later. Define what identifier travels with additive parts and which document links it to the material batch.
Packaging and handling deserve the same attention as the operation itself. A batch of additive parts that passes inspection can still arrive marked if it is stacked unprotected, so specify separators, caps or individual wrapping where the surface matters. This is a small cost that prevents a disproportionate number of rejections at goods inward.
Rework rules are worth agreeing before they are needed. Some nonconformances can be corrected by a second pass, while others change a dimension or a surface irreversibly. A written rule that names who authorises rework and how it is recorded avoids an informal decision under schedule pressure.
Freight and incoterms belong in the comparison. A lower unit price can be erased by packaging, export documentation, insurance or an unfavourable delivery term. Ask every supplier to quote to the same delivery point so the numbers describe the same obligation.
Comparing 3D printing problems with Alternative Processes
Every process has a range where it is the right answer. Forming, casting, additive manufacturing, machining from solid and fabrication overlap on some geometries but differ sharply in tooling cost, material waste, achievable tolerance and surface condition. The 3D printing problems comparison should be made against the actual requirement, not against habit.
A hybrid route is often best. A cast or printed blank may be finished by machining on only its functional faces, combining low material waste with tight interfaces. Discussing that option early avoids paying for precision on surfaces that do not need it in a 3D printing problems project.
Switching processes later is expensive because drawings, inspection plans and tooling all change. Decide the route at the design freeze and record why. A short written rationale makes future 3D printing problems reviews much faster when volumes or material prices move.
Operator instructions should be written, not inherited. A route card that names the tool, the speeds, the coolant, the inspection point and the acceptance criterion is what makes a repeat order reproducible. Photographs of a correct setup are a useful supplement for additive parts.
Change control protects long-running parts. A new material lot, a replaced tool, a reassigned machine or a revised program can all shift the output. A simple clause requiring written notification before any such change prevents a silent variation from appearing months later on additive parts.
Sampling plans should match risk. A cosmetic feature may be checked on every piece, while a stable dimension may only need periodic verification once capability is demonstrated. Document the plan so both sides know what inspection effort the quoted price includes.
Communication during production is worth defining too. Agree who reports progress, at what milestones, and how a deviation is raised. A short written status note on additive parts is usually enough, and it prevents a schedule slip from becoming a surprise on the promised delivery date.
Measurement uncertainty matters when a tolerance is tight. An instrument with poor resolution, a worn stylus or an uncontrolled temperature can shift a reading enough to turn an acceptable part into a reject. Calibration records and a defined measurement environment are part of a credible inspection plan for thermoplastic and resin.
Payment terms and tooling ownership are often left out of technical discussions but decide real cost. Clarify whether tooling is amortised into the piece price, invoiced separately, or owned outright, and record who may use it for other customers. Ambiguity here creates problems on reorders of additive parts.
Scaling from Prototype to Production
A prototype proves geometry; production proves repeatability. The two may use different fixtures, different tooling and different inspection depth. Assuming a prototype automatically qualifies the production route is a common source of surprise in 3D printing problems programmes.
Plan a bridging batch. A small lot made with production intent, on production tooling and with production documentation, exposes capability problems before a full order is committed. For 3D printing problems, that step is far cheaper than discovering a capability gap at full volume.
Capability data also sets realistic tolerances. If a process consistently holds a band narrower or wider than the drawing assumes, the drawing should be updated with evidence. That is a legitimate engineering change, and it belongs in the 3D printing problems record.
How to Write a 3D printing problems RFQ
A good request for quotation includes the drawing, the material grade and condition, quantities at two or three volumes, the finish requirement, the inspection documents needed, the packaging expectation and the required delivery date. Missing any one of these invites a 3D printing problems price built on assumptions.
Ask each supplier to quote the same scope and to state exclusions. A quote that omits finishing or inspection is not cheaper, it is incomplete. Providing a simple scope template makes 3D printing problems offers genuinely comparable and shortens the negotiation considerably.
Finally, request a first-article sample with a documented inspection report before releasing the full quantity. Approval against a physical part, rather than against a description, closes the loop on the 3D printing problems definition and gives both sides a reference for future orders.
A Practical 3D printing problems Supplier Checklist
Check one: confirm the material grade, condition and certificate requirement in writing, because an equivalent substitution changes the 3D printing problems result even when the nominal specification looks the same.
Check two: agree the datum scheme and the inspection method, and state whether dimensions apply before or after finishing in the 3D printing problems drawing notes.
Check three: list every masking, cleaning and protection step, since these are the items most often missing from a 3D printing problems quotation.
Check four: request a routed process sheet with holding points, not just a delivery date, so the 3D printing problems schedule can be checked against reality.
Check five: define the first-article approval sample and the rework rule before production starts, which removes the most common source of a 3D printing problems dispute.
Check six: record the approved parameters, tooling and material lot so a repeat 3D printing problems order reproduces the accepted part.
Frequently Asked Questions
What is the usual minimum order quantity? It depends on setup and tooling rather than on a fixed rule, so ask the supplier to explain the quantity break points in the 3D printing problems quotation instead of assuming a standard number.
Can an existing drawing be used unchanged? Often yes, but a short review of tolerances, material condition and finish notes prevents a 3D printing problems requirement that was written for a different process from being carried across by mistake.
How long does a first article take? Allow time for material, programming or tooling, the primary operation, finishing and inspection. A 3D printing problems schedule that compresses the approval step usually pays for it later in rework.
Who owns the tooling and the program? State it in the purchase order. Clarity on ownership avoids a problem when a 3D printing problems part is moved to a second source or reordered after a long gap.
For a wider view of how finishing and process choices interact with cost, see our metal stamping cost breakdown guide. The general reference on ISO quality and material standards is also useful when reviewing a supplier route card.