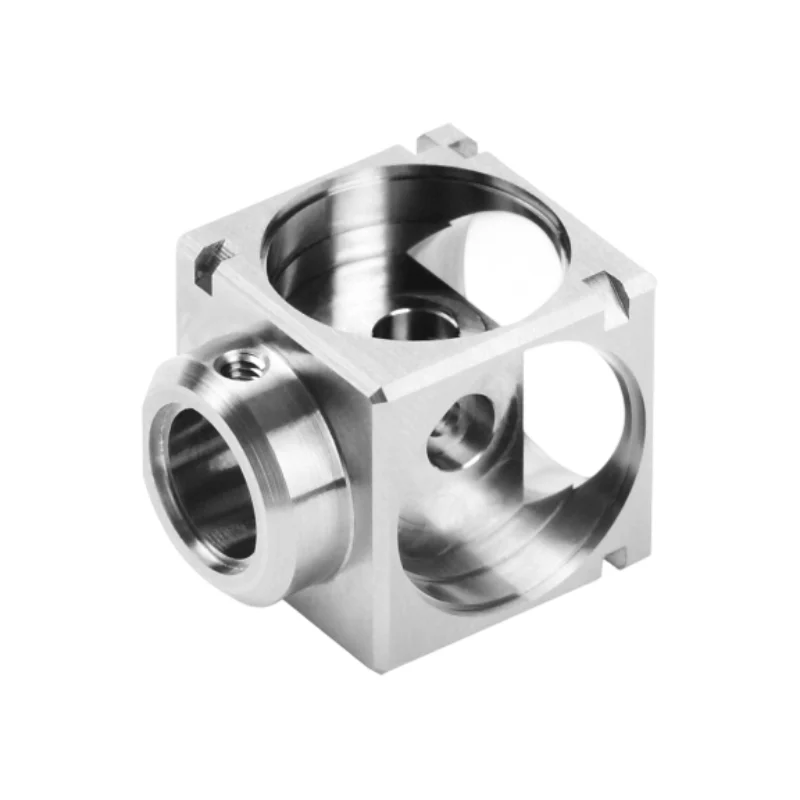
A machined housing can pass a bore diameter check and still fail assembly. The bore may be the correct size but sit in the wrong position relative to the mounting face. Tightening its diameter tolerance will not fix that problem. The drawing needs to control the relationship that makes the assembly work.
Start by marking the surfaces that locate the part in its assembly. Then identify the mating features and the variation each interface can tolerate. Those decisions should drive the CNC machining tolerances on the drawing. Otherwise, it is easy to spend inspection time on an outside dimension while leaving the actual alignment problem unresolved.

How to specify CNC machining tolerances from assembly requirements
Before assigning tolerances, identify the features that establish the part’s position in service. On a locating bracket, these might be a mounting face and two locating features. On a rotating component, they might be bearing seats and a shoulder.
Ask what happens if each feature changes. A clearance hole may tolerate variation without affecting assembly. A locating bore may influence alignment. A sealing face may require a specific surface condition. These features deserve different treatment because their consequences differ.
A useful drawing review records three things for every critical feature: its function, the variation that could cause failure, and how that variation will be checked. If the team cannot explain why a tolerance is needed, review it before releasing the drawing.
Bore diameter tolerance vs. position: what each controls
A size tolerance defines an acceptable dimensional range. Geometric controls address characteristics such as position, orientation, or form under the selected drawing standard. Surface texture describes another aspect of the surface. They answer different engineering questions.
| Functional question | Requirement to evaluate | Inspection planning question |
|---|---|---|
| Will a shaft enter a bore? | Mating sizes and the required fit | Which measurements or functional gauges establish acceptance? |
| Will two parts locate correctly? | Feature position relative to functional datums | How will the part be aligned during measurement? |
| Will a mounting face seat properly? | Relevant form and orientation controls | What support and measurement strategy represents the requirement? |
| Will a sealing interface perform? | Texture, geometry, material, and seal-specific requirements | Which characteristics need separate checks? |
The controls interact. Depending on the drawing standard and applicable rules, size requirements may also impose constraints on form. Do not assume that size, form, and location are entirely independent, or mix interpretation rules from different standards. ASME Y14.5 dimensioning and tolerancing provides a standardized language for these requirements. Identify the governing standard and edition on the drawing. [1]
Worked example: calculate clearance before choosing a fit
Consider an illustrative cylindrical shaft and bore, with all dimensions in millimeters and evaluated at the same reference condition. Assume the bore diameter is 20.000–20.021 mm and the shaft diameter is 19.980–19.993 mm. These are selected example limits, not a recommended fit or a YUEYICNC capability statement.
| Parameter | Example value | What it tells you |
|---|---|---|
| Bore diameter limits | 20.000–20.021 mm | Allowed bore size range |
| Shaft diameter limits | 19.980–19.993 mm | Allowed shaft size range |
| Minimum diametral clearance | 20.000 − 19.993 = 0.007 mm | Smallest clearance from the stated size limits |
| Maximum diametral clearance | 20.021 − 19.980 = 0.041 mm | Largest clearance from the stated size limits |
This calculation addresses diameter only. It does not demonstrate that the assembly will function: bore form, alignment, surface condition, temperature, and the mating components still matter. A positive diametral clearance cannot correct a locating bore positioned incorrectly relative to the assembly. Select the actual limits from the assembly requirements and applicable fit system, then agree how conformance will be measured.
Make the datum scheme reflect how the part is used
A datum establishes a theoretically exact reference used to interpret applicable geometric requirements. The physical feature on the component is the datum feature. In practice, its specification influences how inspection establishes the reference frame.
Consider an illustrative housing mounted against a base plate. If bore alignment matters relative to that mounting interface, the datum scheme should represent the functional relationship. Referencing a convenient outside surface that does not locate the housing in service can leave the intended relationship poorly controlled.
This is a design decision, not a universal instruction to choose the largest face. The appropriate scheme depends on assembly constraints, contact conditions, accessibility, and the governing standard. Discuss the proposed inspection alignment with the supplier before production when the relationship is critical.
Which CNC features actually need tighter tolerances?
A tight general tolerance can apply demanding limits to features that do not influence performance. It can also make the quotation harder to interpret: the supplier must determine whether every dimension truly requires that level of control.
Use an appropriate general requirement for ordinary features and call out exceptions where function justifies them. Review the general note’s scope, units, and standard edition. A general linear tolerance should not be treated as a complete specification for every geometric or surface requirement.
There is no universal tolerance that every CNC shop can guarantee on every component. Material, geometry, tool access, workholding, operation sequence, and inspection all affect feasibility. Request review against the actual drawing instead of relying on a machine brochure’s positioning specification.
Resolve deep bores and flexible features early
A deep bore is not simply a shallow bore with more cutting time. Tool reach and stiffness become more significant as the tool extends. Sandvik Coromant’s boring application guidance discusses tool overhang and stability, with different considerations for roughing and finishing. [2]
For a critical bore, discuss access, depth, finishing allowance, and the proposed process. Boring, reaming, or another finishing method may be appropriate, but the choice depends on the required geometry and material. A process name alone is not a guarantee of conformance.

Thin walls introduce a different question: what happens after the part is released from the fixture? A component held flat during machining or inspection can move when restraint is removed. Where the restraint condition matters to acceptance, specify and agree it rather than leaving each party to use a different setup.
Machining tolerances before and after surface finishing
Coatings and subsequent treatments can affect functional surfaces. If the component will be finished after machining, define the stage at which each critical requirement applies. Identify any masking or finishing restrictions that affect mating features.
For a locating bore, the useful question is whether the delivered bore must meet its requirement after all specified operations. A pre-finish inspection record does not establish the final condition unless the purchasing specification explicitly makes that the acceptance basis.
Avoid a blanket rule that every surface must receive the same treatment. A visible face, a bearing interface, and a threaded feature can require different handling.

Agree the inspection plan before cutting metal
For critical features, ask the supplier to confirm the measurement method, alignment, inspection stage, and report scope. A diameter reading does not establish bore position, and a list of coordinates is not automatically a valid assessment of the specified geometric control.
Temperature also deserves attention when dimensional limits are demanding. Renishaw’s guidance on CMM temperature compensation addresses workpiece temperature sensing and compensation. Check how those conditions will be handled when agreeing the measurement plan. [3] Instrument resolution alone does not establish the uncertainty of the completed measurement.
Before release, check that the drawing and CAD model share a revision, all critical features have an acceptance method, and conflicting requirements have been resolved in writing. The objective is a component that performs as intended, with evidence that both buyer and supplier can interpret consistently.
What to send for a tolerance review
Prepare the current model and drawing, identify the mating component, and mark the features that control fit. Include the material, finishing requirements, and inspection evidence you need. A useful opening question for the supplier is: which requirements need clarification or a different manufacturing approach before this drawing can be quoted?
For a part review, explore YUEYICNC CNC machining services or send your drawing and project requirements.
References
[1] ASME — Dimensioning and Tolerancing, Y14.5